 EN
 AR
 BG
 HR
 DA
 NL
 FR
 DE
 EL
 HI
 IT
 JA
 KO
 PT
 RU
 ES
 SV
 TL
 ID
 SR
 SK
 UK
 VI
 ET
 HU
 TH
 TR
 MS
 GA
 BE
 HY
 KA
 LO
 LA
 MN
 NE
 SO
 MY
 KK
 UZ
Pellet 3D Printing: How to Optimize Extrusion Flow
Pellet 3D printing is becoming an increasingly popular solution for large-scale manufacturing by adding layers of materials through 3D printing. In contrast to ordinary 3D printing which is based on filaments, pellets extrusion printers use plastic granules as a material which offers higher material flexibility, reduces costs of materials, and the amount of the extrusion is significantly higher.
Yet, to keep extruding material consistently, you have to ensure that you get good print quality. A variation in material delivery can cause the layers to be of uneven heights, the surface appearance to be bad, the adhesion between layers to be weak, and the dimensions to be off.
Now, how can a manufacturer make sure that he/she gets consistent material flow from pellet 3D printing? Here are five main points that he/she must be aware of.
1. Set the Right Extrusion Temperature
Temperature is one of the most important factors affecting pellet extrusion performance. If the temperature is too low, plastic pellets may not fully melt, causing excessive extrusion resistance and inconsistent material flow. On the other hand, excessive heat can cause material degradation and affect the final part quality.
Different materials require different processing temperatures. PLA, ABS, PETG, and other engineering plastics should be processed according to their specific material properties.
For better results, use the recommended temperature range as a starting point and make gradual adjustments based on actual extrusion performance.
2. Optimize Screw Speed
In a pellet 3D printer, the screw or extruder regulates the speed at which the plastic pellets are conveyed, melted, and pushed through the nozzle.
A low screw speed may mean the material output is less than the printing speed demands. When you go the other way at high screw speed, the material may not have enough time to melt fully, potentially leading to uneven extrusion or excessive pressure.
Getting the right balance is the essence of the game. It all boils down to screw speed matching nozzle movement speed. Synchronized parameter management will be your best bet for ensuring the extrusion rate remains steady during the printing process.
3. Maintain Consistent Material Feeding
Stable pellet feeding is essential for continuous extrusion. Irregular pellet size, moisture, contamination, or inconsistent feeding can interrupt the material supply and cause fluctuations in extrusion flow.
To avoid these problems:
Use clean, uniform plastic pellets.
Dry moisture-sensitive materials according to the manufacturer's recommendations.
Keep the feeding system free from blockages.
Check the hopper and material supply during long printing jobs.
A reliable feeding system helps ensure that the extruder receives a consistent supply of raw materials.
4. Match Extrusion Flow with Printing Speed
A typical issue that happens with pellet 3D printing is adjusting how much material is being produced versus the moving speed of the print head.
When the flow exceeds the amount needed, over-extrusion will happen, resulting in a large excess of material and an unsmooth finished product. On the other hand, if the flow is too little, then there will be voids between the printed lines, and the layers will not bond well.
The adjustment of nozzle size, layer height, line width, screw speed, and printing speed together will lead to the best results for pellet 3D printing.
When printing big parts on a 3D printer, a good rule is to keep the printing speed reasonably constant to avoid abrupt changes in the flow of material.
5. Monitor and Calibrate the Extrusion System
Regular calibration helps maintain stable extrusion performance over time. Before starting a large printing project, it is useful to conduct an extrusion test and measure the actual material output at different screw speeds.
Operators should also monitor key parameters, including:
Extrusion temperature and temperature stability
Screw rotation speed
Material output rate
Motor load and extrusion pressure, where available
Nozzle condition and material flow consistency
By recording and comparing these parameters, operators can identify potential problems early and adjust the printing settings more accurately.
Conclusion
Optimizing extrusion flow is essential for achieving reliable results in pellet 3D printing. Temperature control, screw speed, material feeding, printing speed, and regular calibration all play important roles in the extrusion process.
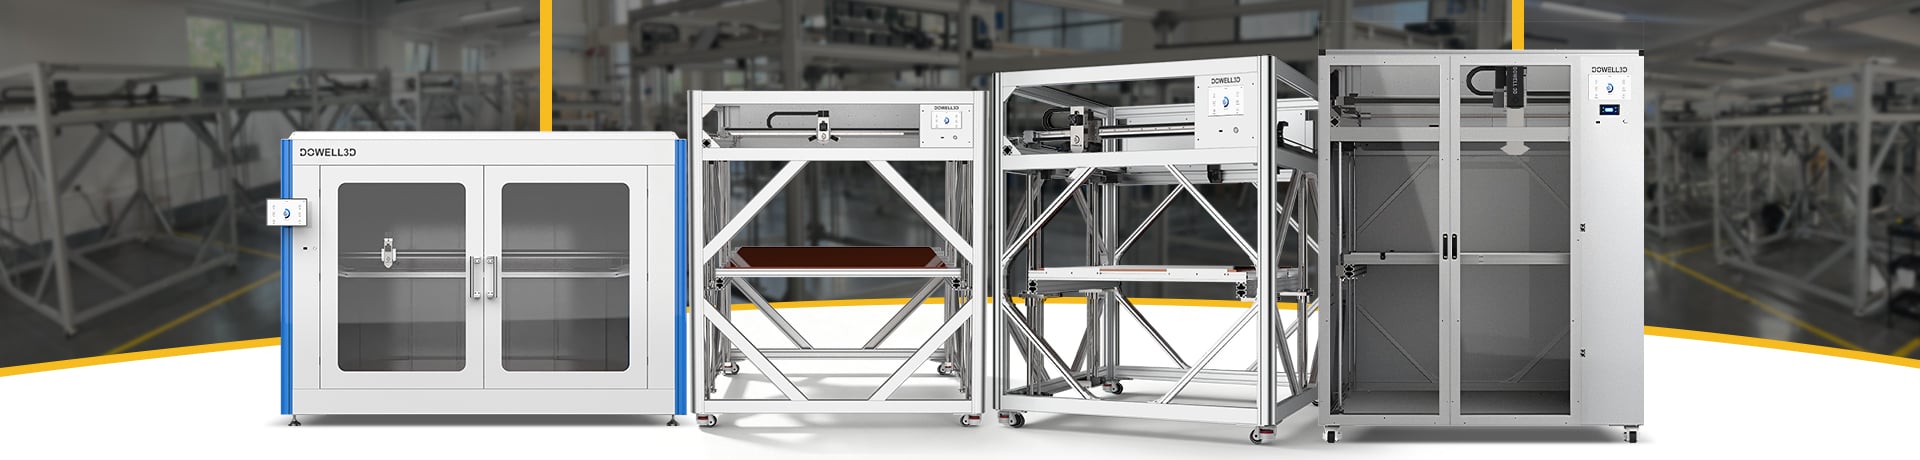
For manufacturers using industrial FGF 3D printers, a well-designed pellet extrusion system can improve material utilization, increase production efficiency, and support the printing of large and complex parts.
The goal is not simply to achieve a higher extrusion rate, but to maintain a stable and consistent material flow throughout the entire printing process.